Mach3

Before discussing Mach3, let us briefly summarize the history of the creation of numerical control and the application of G-code.

The principle of numerical control with G-code (or ISO code)

With the emergence of computerized numerical control, the Massachusetts Institute of Technology (MIT) in the USA developed G-code in the 1950s, which became the most widely used programming language in the world of numerical control.
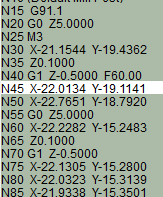
ISO code is primarily composed of G-code lines

More generally, ISO code, consisting of G-commands (as well as M, F, and S commands), allows you to instruct computer-controlled machines, such as milling machines, on what to do and how to do it. G-code commands are instructions indicating where to move, at what speed, and along which path, primarily using two methods: linear or circular interpolation.

Controlling your CNC machine with Mach3

It is possible to create a fully customizable interface by generating G-code, also through LazyCam or Wizards, in addition to customizing M-codes and macros using VBScript. MACH3 software also features spindle speed control, multiple relay control, video display, and manual pulse generation, with support for full-screen mode and touchscreens. This software is feature-rich and offers great value according to your numerical control software needs.
Mach3 turns your computer into a numerical control station

MACH3 runs on most Windows computers to control stepper motor movement using G-code. The required computer specifications are not very demanding, and it can run smoothly on older computers. Pentium, Dual Core, or Core 2 Duo microprocessors are sufficient to run this software. The MACH3 installation is simple and can operate in “demonstration mode” for testing until it is unlocked by a license file, which we offer on our website.

In summary, despite including several advanced features, it is the most intuitive CNC control software available for milling machines. This is why our milling machines are compatible with MACH3.

Servo motor/stepper motor: what is the difference?

Both the servo motor and the stepper motor are DC electric motors. Their high stall (or start-up) torque makes them among the most commonly used motors for robots and special-purpose machines. These motors are also used to drive the axes of CNC milling machines.

The stepper motor

The stepper motor is better suited to small machining operations. Its simple design makes it easy to manufacture and reliable.
However, if the forces applied to the rotor are greater than the motor’s maximum permissible torque (N·m value specified by the manufacturer), a step-loss phenomenon occurs: the motor moves unintentionally and you hear small “cracks” inside the motor.
If you are milling a workpiece made of a hard material and the feed rates of your milling machine are poorly set, the stepper motors driving your axes will be subject to step loss. You will observe the same phenomenon if the speeds and accelerations of your axis movements are too high.

The issue is that during a long machining process, the accumulation of successive step losses leads to large offsets on your milling machine’s axes. The cutter is no longer guided to the originally intended position, and your finished part is no longer acceptable.
For milling small parts and short processes in soft materials, stepper motors are sufficient. However, for producing large parts, they are no longer suitable.

Servo motor

The servo motor is built like a stepper motor, with the difference that it also has an encoder. This allows it to continuously measure the rotor’s rotational speed. The controller can therefore determine whether the rotation command has been fully executed. In the event of step loss, it detects that the motor has rotated less than planned and immediately adjusts the movement. This avoids delays during the machining process.
As a result, the servo motor is not susceptible to step loss and is therefore better suited to milling large dimensions. A milling machine equipped with servo motors can withstand high accelerations and high axis traverse speeds while maintaining positioning accuracy. They are therefore recommended for producing large parts that require high precision.